
Five years ago, few module makers had even heard of EPE. Today, it is close to becoming the most used solar panel encapsulant on the market. EPE encapsulant grew from a 5% market share in 2019 to 38% in 2024, while EVA held 42% (pv magazine). That is a fast shift for a material most buyers never see. It sits inside the module, wrapped around every cell. Yet it shapes how long a module lasts and how much energy it makes.
At Raynex Solar, we manufacture EPE alongside EVA and POE, so we see where each one fits and where each one falls short. In this guide, we explain what EPE encapsulant is and how its three layers work. We also cover its key properties, typical specs, and the modules it suits best. Unlike most supplier articles, we also name the limits you should check before you buy. By the end, you will know if EPE is the right choice for your next production run.
Before we look at EPE, it helps to know what any encapsulant does. A solar module is a stack of layers: glass on top, then encapsulant, then the cells, then more encapsulant, then a back glass or backsheet. The encapsulant is the soft, clear film that melts and bonds this stack into one solid unit during lamination. These polymer layers provide electrical insulation and mechanical support, and they guard cells against moisture, heat, and UV light (TaiyangNews). If the encapsulant fails, the module fails, no matter how good the cells are. That is why we treat it as one of the most important parts of the bill of materials.
A good solar panel encapsulant does eight jobs at once, and it has to keep doing them for 25 years or more. Here is what each one means inside a working module.
The encapsulant wraps around every cell and ribbon and locks them in place. Its strong bond and tensile strength stop cells from shifting during transport, installation, and daily heat cycles. This helps prevent micro-cracks, which can grow over time and cut module output.
The encapsulant acts as a protective layer between the cells and the outside environment. By staying clear and stable, it helps the module deliver steady output year after year. A weak encapsulant may look fine at first, but its losses add up over the life of the module.
The encapsulant is the glue that holds the glass, cells, and backsheet together as one solid unit. This bond gives the module the strength to handle wind, snow, and hail. Without it, the layers would act separately and fail much sooner.
Moisture is one of the main causes of module failure. The encapsulant slows water vapor from reaching the cells, which helps prevent corrosion of the metal contacts. It also helps avoid delamination, where layers start to peel apart.
Solar modules can run at 60°C or more on a sunny day. A good encapsulant stays stable at these temperatures without softening, bubbling, or losing its bond. It also cushions the cells against the stress of heating up by day and cooling down at night.
When the encapsulant protects the cells well, modules suffer fewer faults in the field. That means fewer site visits, fewer module swaps, and lower repair bills. Over a plant’s life, a better encapsulant often pays for itself through lower upkeep.
The encapsulant also helps move heat away from the cells and out through the glass. Cells lose efficiency as they get hotter, so letting heat escape helps protect output. It also lowers the risk of local hot spots that can damage cells.
Sunlight carries UV rays that slowly age plastics and other materials inside the module. A quality encapsulant contains UV stabilizers that resist yellowing and breakdown. This keeps the film clear and protects both the cells and the backsheet from early aging.
No single material does all eight jobs perfectly. Each one trades some strengths for others. That trade-off is exactly why EPE was created.
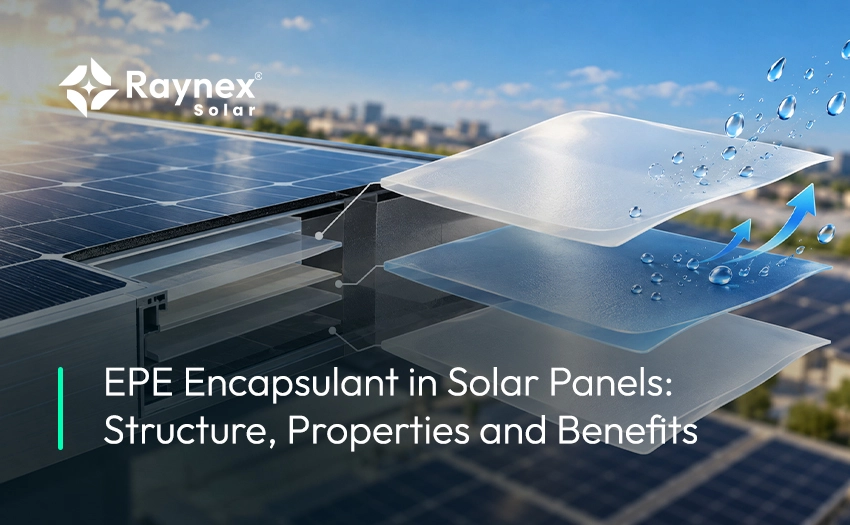
EPE encapsulant is a three-layer solar encapsulant film made of a polyolefin elastomer (POE) core sandwiched between two layers of ethylene vinyl acetate (EVA). The three layers are made together in one step through co-extrusion, so they leave the factory as a single roll. Module makers use it just like any other encapsulant sheet, placing it above and below the cells before lamination. The goal is simple: get the moisture and electrical protection of POE with the easy bonding and processing of EVA. You may also see it called an EVA POE EVA encapsulant, co-extruded encapsulant, or EPE solar film.
EPE is short for EVA-POE-EVA, which describes the layer order from top to bottom. The outer letters are the EVA skins that touch the glass and cells. The middle letter is the POE core that does most of the protective work. Some studies use the broader name “EVA-polyolefin-EVA,” because not every core is a classic POE (TaiyangNews). In everyday trade, though, EPE means an EVA-POE-EVA sheet.
EPE exists because both of the older materials have real weak spots. EVA is cheap and easy to laminate, but it has low PID resistance and can release acetic acid as it ages. POE solves those problems, but it is harder to process. It can trap bubbles during lamination, needs roughly six more minutes per lamination cycle, can let busbars shift during cooling, and bonds less well to glass than EVA (TaiyangNews). Suppliers combined the two to keep the strengths and limit the weak spots. Many EPE grades also use acid-free EVA in the outer layers to cut the acid risk.
The value of EPE comes from giving each layer one clear job. The outer layers handle bonding. The core handles protection. Together, they act like one film, but each part is tuned for what it touches. Here is how the stack works, from the outside in.
The two EVA skins are the parts that touch the glass, the cells, and the ribbons. EVA bonds well to these surfaces, which is why it has been the industry standard for decades. In EPE, the outer layers give the adhesion that pure POE struggles to reach (TaiyangNews). A study of four commercial EPE films found their EVA skins were very alike, with vinyl acetate content of about 25% to 29% TaiyangNews. These skins also keep lamination close to what EVA lines already know. That means less retraining and fewer process changes on the factory floor.
The POE core is the barrier layer. It slows water vapor far more than EVA does, and it blocks the ions that cause PID. Research by Dow and NREL found that POE’s strong PID resistance comes from its resistance to sodium ions moving through it (NREL/OSTI). Because the core sits right in the middle, every path from the glass to the cell has to cross it. POE also does not form acetic acid as it ages. So the core adds protection without adding new chemical risks.
Suppliers can change how thick each layer is. Common EVA/POE/EVA ratios include 1:2:1 and 1:1:1 (Couleenergy). A thicker core gives more barrier, while thicker skins give more bonding. Across commercial films, EVA makes up about 42% to 64% of the total film volume TaiyangNews. All three layers are formed at once through co-extrusion, which is more complex than making a single film. Edge trims from this process can’t be recycled, which is one reason EPE costs slightly more to make than single-layer film TaiyangNews.
The real test of any EPE encapsulant film is how it behaves inside a module. Below are the five properties that matter most to module makers. For each one, we share what independent research has found, not just supplier claims. Where results vary between brands, we say so. That variation is one of the most important things to understand about EPE.
This is EPE’s biggest advantage over EVA. Moisture is measured as water vapor transmission rate (WVTR), and lower is better. In a 2026 study, four commercial EPE films showed WVTR between 3.1 and 11.7 g/m²/day per 100 µm, compared with about 35 for EVA (TaiyangNews). Some EPE grades even matched or beat single-layer polyolefin. That means less water reaching the cells, less corrosion, and less risk of delamination. For moisture-sensitive cells like TOPCon, this is often the main reason to choose EPE.
The POE core gives EPE much stronger electrical insulation than EVA alone. High insulation keeps stray currents from flowing between the cells and the grounded frame. It also blocks the sodium ions that drive potential induced degradation. Industry tests rank EPE between the two other materials: POE gives the highest reliability, EPE comes next, and EVA comes last (TaiyangNews). For many high-voltage modules, that is a clear step up from EVA, though you should still confirm it with PID test data at your system voltage. We cover this in depth in our guide to PID in solar panels.
An encapsulant must stay clear, or the cells lose light. Most EPE grades perform well here. In the same study, three of the four EPE films passed 90.5% to 93% of visible light (TaiyangNews). The fourth film reached only about 86.5%, because its core was more crystalline and turned hazy after lamination. That gap is a clear reminder to check transmittance data for each grade, not just the material name.
Thanks to its EVA skins, EPE bonds well to glass and cells and runs much like EVA on the laminator. Typical lamination time sits near 450 seconds, compared with about 600 for EVA and 300 for single-layer POE (TaiyangNews). In our experience, most lines can switch to EPE with small recipe tweaks rather than new equipment. Peel strength should still be tested after damp heat, because a good bond on day one is not enough. Long-term adhesion is the property that matters most in the field.
The polyolefin layer improves heat resistance compared with EVA alone. Researchers also found that co-extrusion made most EPE films more stable in size than pure EVA, meaning they shrink and swell less with heat (pv magazine). Less movement means less stress on cells during daily heat cycles. Over time, that can help reduce cell cracks and delamination. One film with a non-crosslinking core was the exception, showing more shrinkage and expansion.
Spec sheets are where buyers compare one EPE solar encapsulant with another. The table below shows the typical values for Raynex Solar EPE, along with what each one means on the production line. Use it as a starting point when you read any supplier’s data sheet. Numbers alone don’t tell the full story, so we’ve added a plain-language note for each. For full test methods and batch data, ask for the complete technical data sheet.
| Property | Typical Value (Raynex EPE) | What It Means for Module Makers |
|---|---|---|
| Structure | EVA / POE / EVA | Bonding layers outside, barrier layer inside |
| Thickness | 0.3 mm to 0.6 mm (customizable) | Thicker film adds cushioning and barrier; thinner film cuts cost and weight |
| Light Transmittance | ≥ 90% | More light reaches the cells, so module output stays high |
| Gel Content | ≥ 75% | Shows the film has cured (crosslinked) properly during lamination |
| Peel Strength | High adhesion | Strong bond to glass and backsheet helps prevent delamination |
| Thermal Stability | Excellent | Film holds its shape and bond through daily heat cycles |
| Moisture Transmission | Low | Less water vapor reaches the cells, so corrosion risk drops |
| PID Resistance | Superior | Lower risk of output loss in high-voltage strings |
Gel content deserves a special mention. It tells you how well the film has cured inside the laminator, and low gel content can lead to creep, bubbles, or weak bonding later. Because EPE has layers that cure at different rates, gel content should be checked for your exact lamination recipe. Our article on EVA gel content explains how to test it. You can find full details on our Solar EPE Encapsulant product page.
EPE sits in the middle of the three main encapsulants on most measures. Tests by several material suppliers and module makers show POE gives the highest reliability, EPE comes second, and EVA comes third, while cost runs the other way (TaiyangNews). The table below sums up the main differences. Values are typical ranges, so always check the data for the grade you plan to buy.
| Factor | EVA | EPE (EVA-POE-EVA) | POE |
|---|---|---|---|
| Structure | Single layer | Three layers, co-extruded | Single layer |
| Moisture barrier (WVTR) | About 35 g/m²/day per 100 µm | About 3 to 12 g/m²/day per 100 µm | Low |
| PID resistance | Lowest | High | Highest |
| Acetic acid during aging | Yes | Possible from EVA skins; lower with acid-free EVA | None |
| Adhesion to glass | Strong | Strong (EVA skins) | Weaker |
| Lamination time | About 600 s | About 450 s | About 300 s |
| Processing ease | Easiest | Easy, close to EVA | Harder; bubbles and busbar shift |
| Relative cost | Lowest | Middle | Highest |
Sources: moisture data from TaiyangNews; lamination times and POE processing issues from TaiyangNews.
One note on lamination time: POE cures faster on paper, but its bubble and slipping problems often slow real production. That is why many factories find EPE the easiest upgrade from EVA. For a deeper look at the other two films, see our guides on what POE encapsulant is and why EVA turns yellow.
EPE solar film has found its place in the newest module designs, where EVA alone falls short and pure POE is harder to run. Its growth has tracked the industry’s shift to n-type cells and bifacial modules. Below are the uses where we see EPE make the most sense. In each case, the reason comes back to the same two needs: strong moisture protection and easy processing.
TOPCon is the main driver of EPE demand today. TOPCon cells are more sensitive to water vapor than older PERC cells, so they need a stronger moisture barrier TaiyangNews. Most TOPCon makers are now using EPE on both sides of the module TaiyangNews. EPE gives them much of POE’s protection without POE’s slower, trickier processing. For a full guide, see our post on encapsulants for TOPCon solar modules.
Heterojunction (HJT) cells have a conductive oxide coating on both sides. That coating bonds poorly to POE but well to EVA, yet EVA alone is not a strong enough moisture barrier for HJT over the long term. EPE solves both problems, which is why some HJT makers have chosen it TaiyangNews. The EVA skins grip the coating, and the POE core keeps moisture out.
Bifacial modules collect light from both sides, often in glass-glass builds. Glass-glass modules trap any acid or moisture that gets inside, so the encapsulant must stay stable. EPE’s moisture barrier and lower acid risk make it a strong fit here. It is also a common choice for transparent-backsheet bifacial designs.
Large plants run long strings at up to 1,500 V, which raises the risk of PID. They also need modules that hold their output for 25 to 30 years to meet financial targets. EPE’s PID resistance and moisture barrier help on both counts. For project developers, it offers a reliability upgrade without the full cost of POE.
Rooftop modules face strong heat, because roofs trap warmth beneath the panels. EPE’s thermal stability and low moisture transmission help modules cope with these conditions. For rooftop brands, EPE is also a way to offer longer warranties with more confidence.
High humidity, salty air, and strong heat all speed up module aging. Much of India faces at least one of these, from the humid coasts of Gujarat and Tamil Nadu to the heat of Rajasthan. EPE’s moisture barrier is a clear advantage over EVA in these regions. For the harshest sites, we sometimes still suggest pure POE, especially for glass-glass modules.
For most module makers, the case for EPE comes down to one idea: better protection with almost no change to the production line. You get a stronger barrier than EVA, and you avoid most of the processing pain of POE. That balance is why EPE has grown so fast. Here are the features we see make the biggest difference in real factories.
At Raynex Solar, we also offer custom thickness and roll sizes to match each customer’s line and module design. Every roll is made in India under strict quality checks, which helps shorten lead times for Indian module makers. You can see the full range on our EPE encapsulant product page.
Since EPE grades vary so much, choosing well takes more than reading a data sheet. Over the years, we’ve seen many module makers approve a film from a sample roll, only to face issues once it hits full production. A short, careful check up front saves a lot of cost later. Here is the checklist we suggest to every customer:
For a deeper look at supplier approval, read our guide on what to check before approving a solar encapsulant supplier. If you run into bubbles or other lamination issues during trials, our post on common solar module lamination problems can help.
EPE encapsulant combines a POE core with two EVA skins to give module makers a strong middle path. It blocks far more moisture than EVA, resists PID much better, and still runs like EVA on standard laminators. That is why it has grown from a niche product to nearly 40% of the market in just a few years. It is now the go-to choice for many TOPCon, HJT, bifacial, and utility-scale modules. But EPE is a broad label, not one product, so grade quality matters as much as the material type. The best results come from checking core chemistry, EVA type, and lamination behavior before you commit.
At Raynex Solar, we manufacture EPE, EVA, and POE encapsulant sheets in India, with custom thickness and roll sizes for each line. If you are planning a switch to EPE or qualifying a new grade, our team can share data sheets, samples, and lamination guidance. Explore our Solar EPE Encapsulant range or request a quote to get started.
EPE stands for EVA-POE-EVA. It describes a three-layer film with a polyolefin elastomer (POE) core between two ethylene vinyl acetate (EVA) layers. The layers are co-extruded into one sheet, so module makers handle it like a single film. Some research papers also call it EVA-polyolefin-EVA.
For most modern modules, yes. EPE blocks far more moisture than EVA and offers much stronger PID resistance, which matters for TOPCon, bifacial, and high-voltage modules. It costs more, though, so a quality EVA can still make sense for cost-led PERC modules at lower voltages. The best choice depends on your cell type, voltage, and warranty goals.
Not in every way. Pure POE usually gives the highest moisture barrier and PID resistance, and it forms no acetic acid. EPE wins on processing, with better adhesion to glass and fewer bubble and slipping problems. Many module makers choose EPE as a balance of protection, cost, and line speed.
The POE core is the main barrier against moisture and sodium ions, which cause corrosion and PID. Placing it in the middle means every path from the glass to the cells must pass through it. The EVA layers on the outside handle bonding, since EVA sticks to glass and cells better than POE. This setup lets each material do the job it does best.
Yes, EPE suits most Indian conditions well. Its low moisture transmission helps in humid and coastal areas, and its thermal stability helps in very hot regions. For the harshest sites, especially with glass-glass modules, pure POE may still be worth a look. We recommend matching the grade to the site climate and running damp-heat tests.
EPE film usually comes in thicknesses from about 0.3 mm to 0.6 mm. Thicker film offers more cushioning and barrier, while thinner film cuts cost and weight. The right thickness depends on the module design, cell type, and glass. At Raynex Solar, we can customize thickness and roll size for each production line.