
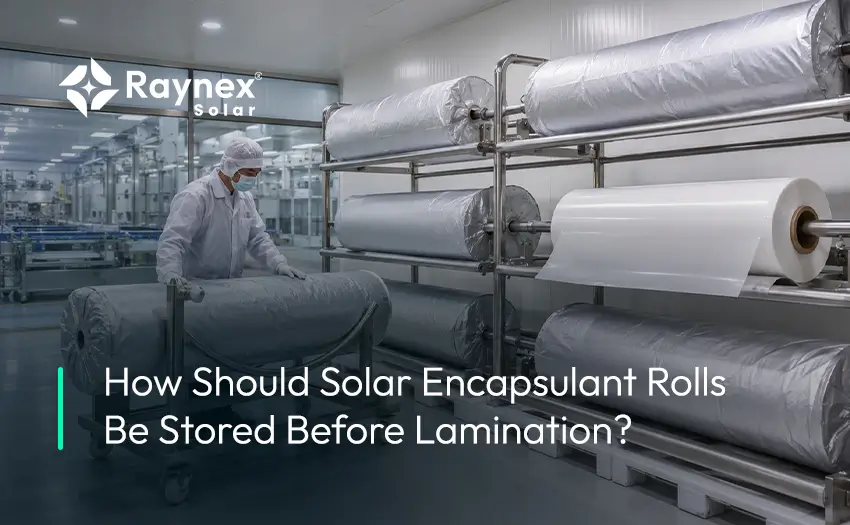
A solar encapsulant roll can arrive at the factory in good condition and still create trouble later if it is stored or handled poorly. Sometimes the problem is obvious, such as damaged wrapping or a crushed edge. In other cases, operators only notice something is different when the film starts unwinding or laying across the module stack.
Raynex Solar manufactures EVA, POE and EPE solar encapsulant sheets for PV module production. Proper storage and handling help maintain the condition of these materials before they reach the layup stage.
Good solar encapsulant storage starts with keeping the roll protected and ready for use until production actually needs it.
Encapsulant film can spend days, weeks or longer in inventory before it reaches the layup station. During that time, heat, humidity, dust and rough handling can affect the condition of the roll. Packaging may get damaged, edges may take pressure, or partially used material may remain exposed longer than intended.
Proper storage helps maintain the condition of the film before it enters the solar module lamination process. If one roll behaves differently from material that previously ran well on the same line, its storage and handling record is worth checking before changing process settings.
The warehouse set point does not tell the whole story. Look at where the rolls actually sit. Material stored close to a loading shutter, hot wall, direct sunlight or a dusty movement area may see different conditions from rolls kept in a cleaner and more stable location.
Humidity also matters after the material moves to production. Once the packaging is opened, shop-floor conditions become part of the handling environment. For solar encapsulant storage conditions, manufacturers should control temperature and humidity while also keeping rolls away from moisture, direct heat and dusty areas.
Do not use one storage rule for every encapsulant in the factory. The encapsulant TDS or technical documentation for the exact grade should define the recommended storage temperature, humidity range, shelf life and any special handling instructions.
EVA films, POE films and EPE films can differ by formulation and grade, so the material-specific requirement should take priority over a general warehouse rule.
A controlled warehouse cannot protect a roll from poor physical handling. Uneven pressure, rough movement or poor stacking can damage the core, edges or protective wrapping. That damage may only become noticeable once operators start unwinding the film.
Roll orientation matters too. If the supplier provides a specific storage position, stacking limit or handling method, use that for the actual roll format. Keep the label visible as well. The grade, batch and roll number should remain easy to identify without opening the packaging.
Open the roll when production needs it, not simply because it has reached the production area. Keeping the packaging intact reduces unnecessary exposure to humidity, dust and accidental contact.
If production uses only part of the roll, protect the remaining film before moving it back to storage. Keep the original batch and roll identification with it so there is no confusion when the material returns to the line.
This does not need to become a long inspection. Before releasing a roll to production, check:
If a roll has already been opened or partially used, keep the original batch and roll identification with the remaining material. Any storage deviation or reopening date should also remain traceable to the same roll.
If anything is questionable, deal with it before the roll reaches layup.
Storage is not the only possible cause of film-handling problems, but it is worth checking when material starts behaving differently.
| What Production May Notice | What Is Worth Reviewing |
|---|---|
| Film waviness | Roll position, storage and handling |
| Unusual surface tack | Storage environment and material condition |
| Dust or marks | Packaging and shop-floor cleanliness |
| Edge damage | Stacking and roll movement |
| Difficult unwinding | Roll condition and unwinder setup |
| Different layup behaviour | Batch details, roll history and process setup |
Machine setup, roll tension and batch variation can produce similar symptoms. If several earlier rolls ran normally and one suddenly behaves differently, check that roll’s condition and handling record before changing the process settings.
No. Storage requirements can vary by material and grade. EVA encapsulant storage conditions depend on the particular EVA grade. The same applies to POE storage and EPE storage.
Even films from the same material family may not have identical handling or shelf-life requirements. When several grades share one warehouse, use the storage instructions for the exact material rather than one common rule for every roll.
Start with the manufacturing date and the shelf life specified for the grade. FIFO helps keep older approved material moving before newer stock, but age alone is not enough.
A roll may still be within its stated encapsulant film shelf life but need review if the packaging was damaged or storage conditions were not maintained. Likewise, a roll that has passed its recommended shelf life should not move into routine production just because the film looks normal from the outside.
QC becomes more important when something falls outside normal storage or handling. The review should focus on the specific reason the roll is being questioned. That may be damaged packaging, a storage excursion, an exceeded shelf life or an unusually long period after opening.
If the material condition cannot be confirmed, hold it for assessment rather than leaving the decision to the layup operator.
Before sending a roll to production, confirm that:
Good solar encapsulant storage is not only about keeping rolls in the right warehouse conditions. It also depends on proper handling, intact packaging, clear traceability and following the storage requirements for the exact EVA, POE or EPE grade.
When these controls are maintained from receipt to layup, manufacturers can reduce avoidable material issues before lamination and keep production more consistent.
It may be possible if the grade-specific instructions allow it. Protect the remaining material and keep its roll and batch identification with it.
Check the handling instructions for the exact grade. If storage and production conditions differ significantly, the material may need preparation before use. Avoid applying one conditioning time to every EVA encapsulant, POE encapsulant or EPE encapsulant.
It can contribute, but storage is not the only possible cause. Roll condition, handling and unwinder settings should also be checked.
Keep the remaining film covered, limit unnecessary exposure and retain the original identification. Follow the handling requirement for that grade before returning it to storage.
Hold it from routine production and review the material specification, storage history and internal quality procedure before deciding whether further evaluation is needed.
Proper solar encapsulant storage helps protect EVA, POE and EPE rolls from moisture, heat, contamination and physical damage before production. Manufacturers should follow the storage and handling instructions for the exact material grade.